Plastics machinery series
Auxiliary equipment
the machines around the press that decide whether parts stay consistent
How well a moulding machine or extruder performs depends on dry resin, accurate dosing and stable cooling water, and all of that is the job of the auxiliaries. This article goes through them one by one, from conveying, drying and dosing to temperature control and granulating scrap for reuse.
Marketing Department, Advanced Chem Solutions · 22 Oct 2026 · 14 min read
Machine overview
Auxiliary equipment is everything around the moulding machine or extruder. Following the resin, it splits into two sides. Before the machine, equipment gets resin to the throat complete, dry and in the right ratio: conveying, dryers, dosers and metal separators. After the machine, equipment controls mould temperature, takes parts out and brings scrap back: temperature controllers, chillers, robots, conveyors and granulators.
Many problems that look like a machine or formulation issue actually start in the auxiliaries: splay because the dryer is exhausted, off-colour because the doser was never calibrated, or a long cycle because cooling water does not flow well enough through the mould.
- Central vacuum conveying — vacuum pump and filter pull resin from bags, bins or the dryer to each machine
- Hopper loader / receiver — receives resin from the conveying line and discharges it into the throat in cycles
- Proportional valve — alternates between virgin resin and regrind by a set time ratio
- Resin dryer — blows hot dry air through a drying hopper to remove moisture from the pellets
- Gravimetric doser — adds masterbatch into the throat at the set percentage
- Magnet / metal separator — catches metal before it reaches the screw
- Robot or sprue picker — removes parts and runners from the mould
- Conveyor — carries parts to inspection or packing
- Beside-the-press granulator — grinds runners and rejects into regrind
- Mould temperature controller (MTC) — circulates water or oil through the mould at a constant temperature
- Chiller — produces chilled water for the mould and other low-temperature loads
- Cooling tower — rejects heat from the water serving the machine's oil cooler and the condenser of water-cooled chillers
Unit by unit
1. Material handling
There are two conveying set-ups. Self-contained loaders with their own pump suit a few machines; a central system uses one large pump with lines and selector valves for many machines. What is often overlooked is the dust and streamers (angel hair) created when pellets rub along the pipe, which can end up as black specks or unmelts in the part.
| Part | Job | What to check on the spec / at acceptance | Symptom when worn or failing |
|---|---|---|---|
| Vacuum pump | Creates the suction that conveys resin | Conveying rate at the real distance and lift · pump type · number of machines served | Cannot keep up, machine runs out of resin at the throat, hot pump |
| Central filter and cyclone | Stops dust before it reaches the pump | Filter cleaning system · dust bin | Falling suction, dust in the pump |
| Receiver | Receives resin and discharges it into the throat | Volume per cycle · built-in filter · discharge flap and level sensor | Leaking flap seal, no pick-up, overflow, blocked filter |
| Proportional valve | Mixes regrind with virgin resin by switching suction time | How the ratio is set · accuracy when the two materials differ in particle size | Regrind ratio fluctuates, colour or properties vary |
| Conveying lines and bends | Route for the resin | Bend radius · pipe material · earthing points | Bends worn through, more dust and streamers, static build-up |
2. Drying
Hygroscopic resins such as PET, PA, PC, PBT, ABS and PMMA absorb water into the pellet, not just onto the surface. Moulded wet, they give splay and bubbles, and in PET, PC and PBT the water also cuts the polymer chains (hydrolysis), so parts turn brittle even when the surface looks fine. These resins need air drier than the surrounding air. Air dryness is expressed as dew point; desiccant dryers typically reach about −40 °C typical reference range — confirm with the machine maker and the TDS.
| Part | Job | What to check on the spec / at acceptance | Symptom when worn or failing |
|---|---|---|---|
| Drying hopper | Keeps resin in hot dry air long enough | Capacity (kg) versus consumption × drying time · insulation · air-spreader cone at the bottom | Resin channels down the middle, part of it is not dried for the full time |
| Desiccant beds or rotor | Remove moisture from the return air to make it dry | Twin-tower or rotating wheel · achievable dew point | Dew point keeps rising, resin is wet although the temperature is right |
| Process and regeneration heaters | Heat the drying air and drive water out of the desiccant | Power · over-temperature cut-out | Drying temperature not reached, desiccant not fully regenerated |
| Process blower | Circulates air through the hopper | Air flow versus resin throughput | Too little air, resin not dry in time |
| Return-air filter and cooler | Stop dust and volatiles before the desiccant | Easy access · return-air cooler for high drying temperatures | Dust and oils from the resin coat the desiccant, which ages quickly |
| Dew point sensor | Measures the actual dryness of the air | Fitted as standard or not · calibration | Wrong readings, nobody knows the dryer is exhausted |
Drying temperatures and times for common resins typical range — follow the TDS of your grade
| Resin | Drying temperature | Drying time | Target moisture |
|---|---|---|---|
| PET | 160–180 °C | 4–6 h | Up to about 0.005 % (50 ppm) |
| PA6 / PA66 | 70–80 °C | 2–4 h | About 0.1–0.2 %; drying too long or too hot causes yellowing |
| PC | 120 °C | 2–4 h | Up to about 0.02 % |
| PBT | 120 °C | 2–4 h | Up to about 0.02 % |
| ABS | 80 °C | 2–4 h | Up to about 0.1 % |
| PMMA | 80–90 °C | 2–4 h | Up to about 0.1 %; lower for clear parts |
| PP / PE | Not hygroscopic and normally not dried, but surface moisture from humid storage, washed PCR or highly filled masterbatch may need warming or a short dry | ||
3. Dosing and blending
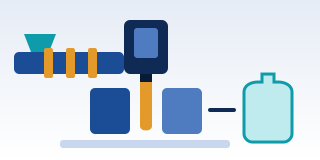
There are three kinds of doser: volumetric, which counts auger revolutions · continuous gravimetric (loss-in-weight), which weighs the MB hopper and trims auger speed · gravimetric batch blenders, which weigh each ingredient into a weigh bin and then mix. The drawing below shows a loss-in-weight unit at the throat.
| Part | Job | What to check on the spec / at acceptance | Symptom when worn or failing |
|---|---|---|---|
| Auger and motor | Deliver MB at the commanded speed | Auger size that puts your kg/h mid-range · fine speed control | Worn auger delivers less per revolution, pellets lodge in the flights |
| Load cell | Weighs the hopper or weigh bin | Resolution · isolation from machine vibration · calibration method | Drift from heat or knocks, the doser corrects in the wrong direction |
| Controller | Compares weight loss with the set point, trims auger speed and logs consumption | Shot mode or screw-recovery mode · data logging · alarms | Wrong mode, dosing out of step with plasticizing |
| Mixing chamber above the throat | Combines MB with the base resin before the screw | Chamber volume · short drop to the screw | MB segregates and reaches the screw in pulses, seen as colour streaks |
| Batch blender (weigh bin and mixer) | Weighs virgin resin, regrind, MB and additives one by one, then mixes | Number of ingredients · batch size versus machine kg/h | Blend segregates on a long route to the throat |
4. Temperature control
Mould temperature controls surface finish, shrinkage, warpage and cycle time. Unpressurised water MTCs reach about 90 °C, pressurised water units about 140–160 °C, and oil units go higher, to about 300 °C typical reference range — confirm with the machine maker and the TDS. Water in the mould channels must flow turbulently (Reynolds number above about 4,000) to transfer heat well; raising the flow rate past this point often helps more than lowering the water temperature.
| Part | Job | What to check on the spec / at acceptance | Symptom when worn or failing |
|---|---|---|---|
| Water MTC | Circulates hot or cold water through the mould at a constant temperature | Maximum temperature · heating and cooling capacity · pump flow and pressure | Mould temperature swings, uneven gloss, scale blockage |
| Oil MTC | For moulds that must run hotter than water allows | Maximum temperature · heat-transfer oil type · high-temperature hoses and couplings | Oil degrades into deposits, poorer heat transfer, leaking couplings |
| Air-cooled chiller | Makes chilled water and rejects heat to the surrounding air | Cooling capacity (kW) at the real ambient temperature · a location with free air flow | Dirty condenser coil, not enough cooling, frequent high-pressure trips |
| Water-cooled chiller | Makes chilled water and rejects heat to cooling-tower water | Cooling capacity · condenser water quality | Scale in the condenser, falling capacity, higher power draw |
| Cooling tower | Rejects heat from the water serving machine oil coolers and condensers | Size versus total heat load · water treatment · blowdown | Hot water, scale, algae, Legionella risk |
| Manifolds and flow meters | Split water into each mould circuit | A flow meter per circuit · scale-resistant material | One circuit blocks unnoticed, parts warp to one side |
5. Size reduction
| Part | Job | What to check on the spec / at acceptance | Symptom when worn or failing |
|---|---|---|---|
| Beside-the-press granulator | Grinds runners and rejects as they leave the machine | Throat opening versus the largest runner · kg/h · slow or high speed · noise | Dusty, hot regrind, noise |
| Central granulator and shredder | Breaks large parts or purgings before fine grinding | Maximum piece size · feeding system | Jams, large pieces hang up |
| Rotor and bed knives | Cut the plastic into pieces | Knife material · gap-setting method | Blunt or wide-gap knives give fines, long strands and heat |
| Screen | Sets regrind size | Hole size, often about 4–8 mm for beside-the-press grinding typical reference range — confirm with the machine maker | Worn, enlarged holes, uneven regrind, unstable feeding into the screw |
| Dust separator | Removes fines from regrind | Fitted or not · dust collection | Fines reach the screw and burn into black specks |
6. Part handling
| Part | Job | What to check on the spec / at acceptance | Symptom when worn or failing |
|---|---|---|---|
| Sprue picker | Picks the sprue or runner and drops it into the granulator | Stroke · speed · mounting on the platen | Missed picks, sprue left in the mould, mould closing on it |
| Servo robot (3 axes or more) | Takes out parts, stacks them, loads inserts or in-mould labels | Payload · axis strokes · mould entry and exit time · interface signals with the machine | Longer cycle because the robot is slow, dropped parts, mould crashes |
| End-of-arm tooling | Holds the part by vacuum or grippers | Quick change with the mould · grip confirmation sensor | Leaking suction cups, marked parts |
| Conveyor | Carries parts away from the machine | Width · speed · cooling time on the belt | Hot parts piling up and warping |
| Fencing and interlocks | Keep people out of the robot zone while it runs | Safety door switches · emergency stops | Bypassed interlocks are a serious accident risk |
7. Metal separation and colour change
| Part | Job | What to check on the spec / at acceptance | Symptom when worn or failing |
|---|---|---|---|
| Magnet drawer | Catches ferrous metal at the throat | Number of bars · easy removal for cleaning | Catches ferrous metal only; build-up eventually washes into the screw |
| Metal separator | Detects all metals, including stainless steel and aluminium, and rejects them | Sensitivity · reject method · mounting position | Sensitivity set too low, metal damages the screw and check ring |
| Colour-change features | Easy-clean hoppers, drain ports and cleaning vacuums | Colour change without stripping many parts | Pigment left in hoppers and dosers, old colour in the new lot |
Machine types
Dryers
| Type | Principle | Strengths | Limits | Best for |
|---|---|---|---|---|
| Hot-air dryer | Heats ambient air and blows it through the hopper | Simple, low investment | Air is as humid as the surroundings; in a humid climate such as Thailand's it only removes surface moisture | PP and PE with surface moisture, preheating resin |
| Desiccant (dehumidifying) dryer | Closed air loop through a desiccant before heating and blowing into the hopper | Low dew point, dries hygroscopic resins to target | Desiccant, filters and regeneration need care; regeneration uses energy | PET, PA, PC, PBT, ABS, PMMA |
| Vacuum dryer | Heats resin, then lowers pressure so water evaporates at a lower temperature | Shorter drying time than desiccant drying for many resins | Batch or rotating stations, narrower throughput range, higher investment | Frequent material changes, hygroscopic resins in moderate quantities |
| Infrared (rotating drum) | Infrared radiation heats the pellet interior in a rotating drum | Fast heating, can crystallise PET in the same step | Specific materials and applications, settings per material | PET flake and pellets, PET recycling |
Dosers
| Type | Principle | Strengths | Limits | Best for |
|---|---|---|---|---|
| Volumetric auger | The auger delivers a fixed volume per revolution | Simple, low investment | Delivered weight changes with bulk density, pellet size and hopper level; recalibrate for every MB or lot change | Colour MB whose result you can see, jobs checked by regular catch tests |
| Continuous gravimetric (loss-in-weight) | Weighs the MB hopper and trims auger speed automatically | Self-correcting when pellets change, records actual consumption | Needs vibration isolation and load-cell calibration, one unit per ingredient | Functional MB (UV, FR, antistatic) and high-value MB |
| Gravimetric batch blender | Weighs each ingredient into a weigh bin, then mixes the batch | Several ingredients in one unit (virgin, regrind, MB, additives), consumption logged per ingredient | Blend can segregate if the route from blender to throat is long | Extrusion and moulding with several ingredients |
How to size the equipment
Every auxiliary starts from the same number: how much resin the machine uses per hour (kg/h). Worked example: shot weight including runner 400 g, cycle 30 s = 120 shots per hour = 48 kg/h.
- Drying hopper Capacity (kg) = consumption (kg/h) × drying time (h), e.g. 48 kg/h × 4 h ≈ 190 kg. Convert to volume using the pellet bulk density, typically about 0.5–0.8 kg/L, so roughly 240–380 litres. A hopper that is too big for a slow-running machine keeps resin in hot air too long and yellows it, especially PA.
- Dryer Air flow and heater power must cover the kg/h and drying temperature of the most demanding resin you will run, not just today's resin.
- Conveying Conveying rate must exceed machine consumption with margin. Capacity drops with longer lines, more lift and more bends; use the maker's curves at the real distance.
- Doser MB per hour = machine kg/h × let-down, e.g. 48 kg/h × 2 % ≈ 1 kg/h. Choose a doser whose accurate range has 1 kg/h in the middle, not one designed for several tens of kg/h.
- Chiller Heat load (kW) ≈ resin throughput (kg/h) × heat removed per kilogram from melt to ejection temperature (kJ/kg) ÷ 3,600, plus hot-runner heat and oil coolers if they share the water. Semi-crystalline resins (PP, PE, PA) need more heat removed than amorphous ones (PS, ABS, PC) because of the latent heat of crystallisation. Get the resin enthalpy figure from the resin or chiller maker.
- Chilled-water flow Litres per minute ≈ 14.3 × heat load (kW) ÷ supply-to-return temperature difference (°C). Chilled-water systems are typically designed for a difference of about 3–5 °C; e.g. 10 kW at 5 °C ≈ 29 L/min.
- Mould temperature controller Choose by required mould temperature (water or oil), heater power to bring the mould up to temperature in time, and a pump that gives turbulent flow in every circuit.
- Granulator Choose by kg/h of runners and rejects and the largest piece it must take. Slow-speed beside-the-press granulators make less dust and noise.
Numbers in this section are typical reference ranges — confirm with the machine maker and the TDS.
Maintenance checkpoints
| Frequency | Checkpoint | What to look at | What happens if neglected |
|---|---|---|---|
| Every shift | Dryer | Dew point, inlet air temperature at the hopper, resin level in the hopper | Wet resin, splay, brittle parts |
| Every shift | Doser | Alarms, MB level, actual consumption versus plan | Under- or over-dosing that nobody notices |
| Every shift | Loaders | Filters, flap seals, resin reaching the throat in time | Throat runs empty, short shots |
| Every shift | Safety | Robot fence and granulator interlocks, emergency stops, no hands into the granulator throat | Serious hand and arm injuries |
| Weekly | Dryer filters (process and return air) | Dust, condensed volatiles | Low air flow, rising dew point, desiccant ageing fast |
| Weekly | Central filter and dust bin of the conveying system | Full dust bin, blocked filter | Falling suction, hot pump |
| Weekly | Throat magnets | Collected ferrous particles | Particles washing into the screw |
| Weekly | MTCs and hoses | Water strainers, leaks, ageing hoses | Hot water or oil sprayed on people, mould temperature swings |
| Monthly | Doser calibration | Check load cells with test weights and collect MB output for a set time and weigh it against the set point | The screen shows the right value while actual dosing is off |
| Monthly | Chiller condenser | Clean coil (air-cooled), scale in tubes (water-cooled) | Not enough cooling, high-pressure trips, higher power draw |
| Monthly | Cooling tower and water quality | Treatment chemicals, blowdown, scale, algae, clean basin | Scale blocking mould channels and oil coolers, Legionella |
| Monthly | Granulator knives and screen | Sharpness, gap per the manual (feeler gauge), worn screen holes | Dust, hot regrind, strands, unstable feeding |
| Yearly or at the maker's hour interval | Desiccant and regeneration | Regeneration performance, replace desiccant at end of life, check tower switching valves | Dew point misses target although everything looks normal |
| Yearly or at the maker's hour interval | Dew point sensor and chiller | Calibrate the sensor; refrigeration circuit checked by a qualified technician | Wrong readings, refrigeration damage |
| Every time equipment is opened | Lock-out/tag-out (LOTO) | Isolate and lock power before opening the granulator; wait for the rotor to stop completely because it keeps turning under its own inertia; lock the rotor before changing knives; beware hot surfaces on dryers, hoppers and oil MTCs | Fingers and hands cut by knives, burns from hot surfaces and hot oil |
Masterbatch and additives on this equipment
Dosing accuracy is money When the doser is not trusted, many plants dose "to be safe", for example setting 2 % when the formulation needs 1.5 %. That means using about a third more MB than needed on every part, every shift. A gravimetric doser and regular calibration let you set close to what the formulation actually needs. Put your own numbers into the cost per good part calculator.
Functional MB should be dosed by weight Under-dosed colour MB is visible; under-dosed functional MB shows nothing at the machine. A part short of UV stabiliser cracks after months outdoors, a part short of FR fails the flammability test, and a part short of antistatic shows dust at the customer. See plastic cracking in sunlight · flame-retardant PP to UL94 V-0 · dust on plastic parts.
Moisture and splay Most splay comes from under-dried base resin, but MB can pick up moisture too, especially MB with high filler, carbon black or hygroscopic additives. Keep opened bags sealed and dry the MB if its TDS says so. How to separate the causes is explained in splay and silver streaks.
Regrind ratio Regrind already contains MB, so if the regrind ratio swings, the actual additive level in the part swings with it. Regrind has also been through at least one heat history and part of its stabiliser is used up. Many plants cap regrind at about 10–25 %, depending on the part and the customer's specification typical industry range — confirm by trial on your own machine. More important than the number is keeping it constant with a proportional valve or batch blender, and drying regrind of hygroscopic resins like virgin material.
Colour change and purging Clean the hopper, doser, mixing chamber and loader before purging the screw, because pigment left in the auxiliaries drops in later as colour streaks. Purge with a purging compound or the base resin, and sequence from light to dark. See colour streaks and black specks.
What additives cannot fix Wet resin from a dryer with exhausted desiccant, colour streaks from an uncalibrated doser and warpage from a blocked mould circuit must be fixed at the equipment. If you want to know whether the let-down you run matches what the formulation really needs, the ACS team can review it through the Free Dosage Audit.
Related process articles
The auxiliaries in this article serve both injection molding and extrusion. Symptoms that often start in the auxiliaries: splay · brittle parts · short shots · warpage.
FAQ
Auxiliary equipment questions we hear often
Is a hot-air dryer enough, or do I need a desiccant dryer?
It depends on the resin. Resins that absorb moisture into the pellet, such as PET, PA, PC, PBT, ABS and PMMA, need air drier than the surroundings, which a hot-air dryer cannot provide in a humid climate such as Thailand's. A hot-air dryer is enough to remove surface moisture from PP and PE or to preheat resin.
Is a gravimetric doser worth it over a volumetric one?
A volumetric doser delivers a fixed volume, so the actual weight changes with bulk density and pellet size, and it must be recalibrated for every MB or lot change. A gravimetric doser corrects itself and records actual consumption. It pays back fastest when the MB is high-value, when it is a functional MB whose effect you cannot see, or when the plant has been over-dosing to be safe. Work out the difference with the cost per good part calculator.
How much regrind can I use?
There is no single number for every job. Many plants cap regrind at about 10–25 %, depending on the part and the customer's specification. More important is keeping the ratio constant, checking part properties whenever the ratio changes, and drying regrind of hygroscopic resins like virgin material.
Can resin be dried for too long?
Yes. PA and some other resins yellow or degrade when kept in hot air too long, and some additives can evaporate. Common causes are a drying hopper too large for the machine's consumption, or a moulding machine that stops for a long time while the dryer keeps running at full temperature. Size the hopper to actual consumption and use a set-back mode when the machine stops.
Caution
General knowledge for understanding only. Numbers are typical reference ranges. Selection, installation, operation and maintenance must follow the machine maker's manual and instructions and your plant's safety rules.
Let-down ratios and technical data on this page are typical reference values, not a guarantee of properties. Confirm by trial in your own process before production use.