Plastics processing
Extrusion
melt pushed continuously through a die to make long parts with a constant cross-section
Pipe, profiles, sheet, film and strapping all come off an extruder. A rotating screw melts the plastic and pumps it through a die that sets the cross-section; downstream equipment then sizes, cools, pulls and winds or cuts it. This article walks through each part, the parameters to control and the defects you see most often.
Marketing Department, Advanced Chem Solutions · 21 October 2026 · about 9 min read
The principle in one minute
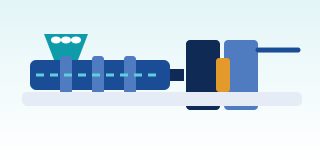
The single-screw extruder is the workhorse of most extrusion. Pellets drop from the hopper into the screw channel, and the screw turns inside a barrel wrapped with heater bands, carrying the material forward through three zones.
- Feed zone deep, constant channel that conveys solid pellets and starts compacting them
- Compression (transition) zone the channel gets progressively shallower, so pellets are squeezed, sheared and melted. Feed channel depth divided by metering depth is the compression ratio.
- Metering zone shallow, constant channel that homogenises the melt, evens out its temperature and pumps it at a steady rate
The heater bands are not the only source of melting energy. A large share comes from the shear work the screw does on the plastic, which is why melt temperature usually rises when you increase screw speed, even with the heater settings unchanged.
Before the die, the melt passes a screen pack (several layers of wire mesh) supported by a breaker plate (a perforated plate). The screens catch contamination and unmelted material and add back pressure that improves mixing. Melt pressure creeping up before the screens means they are clogging. Lines running PCR often fit a screen changer so screens can be swapped without stopping.
The die sets the cross-section: a pipe die has a central mandrel · a flat die (coat-hanger type) is used for sheet and cast film · a spiral annular die is used for blown film. The final shape is fixed downstream, while the plastic cools.
Steps along the line
Extrusion is continuous, so there is no cycle as in injection moulding, but every line has the same seven steps:
- Feed base resin, masterbatch and regrind enter the hopper through a gravimetric blender
- Melt and convey the screw carries the material through the feed, compression and metering zones
- Filter the screen pack and breaker plate catch contamination
- Shape at the die the melt leaves with the required cross-section
- Size and cool Pipe and profile: a vacuum calibration sleeve pulls the outer surface against the sleeve while it cools, followed by spray or immersion water tanks · Sheet and cast film: chill rolls (or a roll stack) cool the melt and give it its surface · Blown film: internal air inflates a bubble and an air ring cools it from outside
- Haul-off a caterpillar puller for pipe or nip rolls for film; haul-off speed relative to die output sets the thickness
- Cut or wind a saw cuts pipe to length, a winder rolls up film and thin sheet; film that will be printed passes a corona treater before winding
Line speed is usually limited by cooling capacity (tank length, chill rolls or frost-line height) or by melt fracture at the die as output is pushed up.
Blown film: BUR and frost line
The melt leaves an annular die as a thin tube, and air introduced inside inflates it into a bubble. Bubble diameter divided by die diameter is the blow-up ratio (BUR). BUR sets the film width and the transverse (TD) orientation, while nip-roll speed relative to die exit speed sets the machine-direction (MD) draw. The two must be balanced, or the film tears easily in one direction.
The frost line is where the film solidifies, visible as a hazy band around the bubble; above it the bubble stops expanding. Frost-line height affects clarity, toughness and achievable line speed. The collapsing frame then flattens the bubble, and the nip rolls trap the air inside and pull the film to the winder.
Parameters to control
| Parameter | What it controls | What goes wrong if it is off |
|---|---|---|
| Barrel temperature profile | Melting, viscosity | Too low: unmelts, gels, pressure swings · Too high: degradation, die build-up, sagging bubble or pipe |
| Screw speed (rpm) | Output and shear heating | Too high: melt overheats or does not fully melt · Unstable: thickness swings |
| Melt pressure before and after the screens | Screen condition and flow stability | Steady rise: screens clogging · Rhythmic swings: unstable feeding (surging) |
| Actual melt temperature at the die | Viscosity at the die and surface quality | Can differ a lot from set points; measure it with a melt probe rather than reading heater settings |
| Die gap and die temperature | Thickness across the width or around the circumference, surface | Uneven transverse thickness; too narrow a gap leads to melt fracture |
| Haul-off speed | Wall thickness and draw-down | Unsteady speed: thick and thin sections |
| BUR and frost-line height | Width, orientation, clarity | MD/TD imbalance, film tears easily one way, unstable bubble |
| Vacuum level and cooling water temperature | Size and roundness of pipe or profile | Ovality, out-of-spec dimensions, dull surface |
| Chill roll temperature | Surface, clarity, flatness | Dull surface, curled sheet, hazy film |
| Winding tension | Roll shape and film blocking | Too tight: blocking · Too loose: telescoping |
Reference melt temperatures: PE about 160–230 °C (LDPE at the low end, HDPE pipe at the high end) · PP about 200–260 °C. Typical range — follow the TDS of your grade.
Typical products and resins
| Product | Common resins | Which way MFI goes |
|---|---|---|
| Pipe (water, gas, cable conduit) | HDPE (PE80, PE100 grades), PP-R, PVC | Very low, often fractional MFI |
| Profiles (edging, frames, channels) | PVC, PP, PE, WPC | Low |
| Sheet for thermoforming | PP, PS/HIPS, PET, ABS | Low to medium; needs enough melt strength for forming later |
| Blown film | LDPE, LLDPE, HDPE and blends | Low; HDPE film is often fractional MFI |
| Cast film | PP (CPP), LLDPE, PET | Higher than blown film |
| Strapping | PP, PET | Low to medium; strap is stretched after extrusion so the chains align and give lengthwise strength |
Which way MFI goes: most extrusion uses lower MFI than injection moulding, because the product has to hold its shape on its own between the die and the point where it sets. Large pipe must not sag, the bubble must stay stable and sheet must not draw down before it reaches the rolls. Cast film and extrusion coating are the exceptions: the melt touches a chill roll almost immediately, so higher-MFI grades work.
PVC is different from the polyolefins. It is usually extruded from dry blend on a counter-rotating twin-screw extruder and needs a heat stabiliser, because PVC degrades readily when hot.
Common defects
Because extrusion runs continuously, a problem does not cost one part, it costs a whole roll or length. First decide whether it is a machine, resin or formulation issue.
| Symptom | Likely cause | How to check | Can an additive help? |
|---|---|---|---|
| Sharkskin surface up to gross distortion (melt fracture) | Wall shear stress at the die exit above the critical value for the polymer: output too high for the die gap, melt too cold, narrow molecular weight distribution grades such as LLDPE | Appears once output passes a certain point and disappears when you slow down or raise temperature | A fluoropolymer processing aid (PPA) that coats the die wall helps clearly. It needs conditioning time before it works, and some antiblocks and pigments reduce its effect, so test the full formulation |
| Die lines along the length | Degraded deposits at the die lip (die build-up), damaged die lip, trapped contamination | Line at a fixed position → die · Disappears after cleaning but comes back → build-up | PPA reduces die-lip build-up, stabilisers reduce degradation. With PCR, see inconsistent recycled resin |
| Gels, fish-eyes | Unmelted material, very high-MW or crosslinked material from hang-up in dead spots, poorly dispersed MB, contamination in PCR | Cut out a gel and heat it under a microscope: if it melts in, it was unmelted or high-MW · if not, it is crosslinked or contamination. Count gels per area and compare lots | Well-dispersed MB with a carrier compatible with the base resin. With PCR, fine filtration is essential — see recycled resin |
| Thickness variation | Along the length: unstable feeding (surging), fluctuating hopper level, mixed pellet sizes, unsteady haul-off · Across the width: uneven die gap, uneven die or air-ring temperature | Measure thickness profiles in both directions; check whether melt pressure swings rhythmically | Mostly machine-side, but MB or PCR with pellet size very different from the base resin can make feeding unstable |
| Film blocking, hard to open | Not enough antiblock, winding while the film is still warm, high winding tension, very smooth surfaces | Unwind and inspect, measure blocking force (ASTM D3354) and COF (ASTM D1894) | Yes — see film sticking together |
| Line instability with PCR | Lot-to-lot MFI swings, moisture, contamination, odour | Measure MFI and moisture on every lot, trend pressure before the screens | See inconsistent recycled resin |
| Outdoor film turns brittle early (agricultural, greenhouse, mulch film) | UV cuts polymer chains; thin film degrades faster than thick parts; agrochemicals containing sulphur or halogens reduce the effectiveness of some HALS | Compare elongation at break of exposed and unexposed areas | Yes — see plastics turning brittle in sunlight |
Additives in extrusion
Masterbatch is added through a gravimetric blender above the extruder throat. This is the most accurate method and it matters more in extrusion than elsewhere: the line runs continuously, so a dosing error turns into a whole roll of scrap.
- Multilayer (coextruded) film put the additive only in the layer that needs it, for example antiblock in the skin layers, and calculate the let-down against that layer, not the whole film
- Slip and antiblock for packaging film — see Slip & Antiblock MB
- UV for agricultural film and outdoor pipe and profiles; black HDPE pipe relies on well-dispersed carbon black as its UV screen — see UV masterbatch
- Antistatic for film and sheet that attract dust — see antistatic masterbatch
- Nucleating agent for PP sheet and cast film that needs stiffness or clarity — see nucleating agents
- PCR in multilayer film or pipe, a PCR core layer keeps the outer surfaces smooth and printable — see PCR resin
- Processing aids and desiccants PPA for melt fracture and die build-up, desiccant for damp PCR
ACS does not extrude pipe, sheet or film for customers. We design masterbatch formulations and produce them with a network of partner compounders; recycled Circular grades are pelletised in ACS's own plant (see how). Where we help is choosing the formulation and let-down for each layer and product, and separating out the problems that have to be fixed at the machine.
FAQ
Extrusion questions we hear often
Why does extrusion use lower-MFI resin than injection moulding?
Once the product leaves the die it is still hot and has no mould to support it, so it has to hold its shape with its own melt strength until it sets. Pipe must not sag, the film bubble must stay stable and sheet must not draw down before it reaches the rolls. Low-MFI grades have higher molecular weight and cope better. Cast film and extrusion coating are the exceptions, because the melt touches a chill roll almost immediately, so higher MFI works there.
How do BUR and frost line affect blown film?
BUR is bubble diameter divided by die diameter. It sets the film width and the transverse orientation, while nip-roll speed sets the machine-direction draw. The two have to be balanced, or the film tears easily in one direction. The frost line is where the film solidifies; its height affects clarity, toughness and the line speed you can reach. Whenever you change one of these, recheck the film properties.
I added slip, so why is freshly extruded film still not slippery enough?
Amide slip agents such as erucamide need time to migrate to the film surface after extrusion, so COF keeps falling over the first several hours to several days, depending on storage temperature, film thickness and corona treatment. Antiblock works immediately because it roughens the surface. Measure COF at the same time after extrusion every time so lots can be compared.
How far can I go with PCR in extrusion?
PCR works in many extrusion jobs, provided you control three things: MFI close to the base resin and stable lot to lot, enough filtration for the contamination, and low moisture. In multilayer film or pipe, putting PCR in the core layer keeps the outer surfaces smooth and printable. Start at a low ratio and step up while checking gels, thickness and mechanical properties.
Technical caution
Let-down ratios and technical data on this page are typical reference values, not a guarantee of properties. Confirm by trial in your own process before production use.
Send us a problem film or part
Send a sample or photos with your resin grade, formulation and layer structure. We will help you tell whether the problem sits in the formulation or at the machine. Free of charge, no obligation to buy.