Plastics machinery series
Blow molding machine (EBM / ISBM)
forms a parison or preform, then blows it against a cold mould
An EBM machine is an extruder with a parison head, coupled to a mould and clamp, an air system and a deflashing station; an ISBM machine is a preform injection unit or reheat oven coupled to a stretch rod and high-pressure air. This page takes the machine apart unit by unit: what to check on the spec sheet, which parts wear first, how to size it and where to look during maintenance.
Marketing Department, Advanced Chem Solutions · 22 Oct 2026 · 13 min read
Machine overview
An EBM (extrusion blow molding) machine has four working groups. The extruder melts the resin. The parison head forms the parison and controls wall thickness. The mould unit pinches, blows and cools. The downstream section trims flash, leak-tests and sends bottles out. All four run on one rhythm: if one is slow, the whole machine is slow.
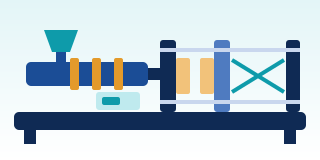
An ISBM (injection stretch blow molding) machine has no parison head. Instead it has a preform injection unit (single-stage) or a preform reheat oven (two-stage), a stretch rod and a high-pressure air system. The drawing below shows a shuttle-type EBM machine, the most common layout in HDPE bottle plants; the ISBM units are covered in table 5.
- Hopper and dosing unit — feeds virgin resin, regrind and masterbatch in set proportions
- Drive and gearbox — turns the screw at steady torque and speed
- Screw, barrel and heater bands — melt, mix and pump the melt at a steady rate
- Parison head (crosshead) — turns the flow and spreads the melt around the mandrel into a hollow tube
- Servo die-gap actuator — moves the mandrel or bushing according to the parison program
- Parison — the hanging tube of melt waiting for the mould
- Parison cutter (knife) — cuts the parison from the head after the mould closes
- Mould, clamp and carriage — pinch off, hold the mould shut during blowing and carry it to the blow station
- Blow pin or needle — injects air into the parison and calibrates the neck
- Deflashing / trimming station — removes neck, bottom and handle flash and sends it to the granulator
- Leak tester — pressurises each bottle, measures pressure decay and rejects leakers
- Take-out conveyor — carries bottles to packing
Unit by unit
Each table has the same four columns. Use them when comparing quotations, at machine acceptance, and when bottles start drifting and you need to find out why.
1. Extruder
The extruder on a blow molding machine is an ordinary single-screw extruder. What differs is the target: blow molding needs a melt that is cool enough and steady, because the parison must carry its own weight. A few degrees too hot and the parison sags and the upper wall thins.
| Part | Job | What to check on the spec / at acceptance | Symptom when worn or failing |
|---|---|---|---|
| Hopper and dosing unit | Feeds virgin resin, regrind and MB in proportion | Gravimetric or volumetric, number of components, accuracy stated by the maker, low-material alarm | Bottle colour goes light and dark in waves; bottle weight drifts when the regrind ratio changes |
| Screw | Conveys, melts, mixes and builds pressure | Diameter, L/D, screw type (barrier, mixing section), material and surface treatment | Lower output at the same rpm, higher melt temperature, unmelted pellets, poor colour mixing |
| Barrel and heater bands | Supply heat and control each zone | Number of zones, heater type, cooling fans per zone, thermocouple positions | Zone temperatures swing, a dead heater band leaves a cold spot and uneven melting |
| Drive and gearbox | Turn the screw with high torque at low speed | Motor power, maximum torque, drive type (inverter or servo), gearbox cooling | Noise, hot gear oil, screw speed jerks, motor current swings |
| Screen pack and breaker plate | Catch contamination before the head | Screen size, pressure tap ahead of the screen | Steadily rising pressure, black specks or gels in the bottle wall |
2. Parison head and parison programming
The head is the heart of an EBM machine. A crosshead takes the melt in from the side and spreads it around the mandrel so it leaves as a tube with an even wall all round. The opening between mandrel and die bushing at the exit is the die gap, and it sets the parison wall thickness.
Parison programming moves the die gap during extrusion so the parison is thicker where it will be stretched most, such as shoulders, corners and handles, and thinner where it stretches little. The controller divides the parison length into points and sets a gap value at each one; more points means finer control. Current machines move the mandrel or bushing with a hydraulic or electric servo, and some add partial wall thickness control for non-round bottles.
| Part | Job | What to check on the spec / at acceptance | Symptom when worn or failing |
|---|---|---|---|
| Crosshead and mandrel | Spread the melt around the circumference and form the parison bore | Distributor design (heart-shaped or spiral), die size range, number of heads for multi-cavity work | Die lines along the length, one side thin, a weld line along the parison |
| Die bushing and die gap | Set the outer diameter and wall thickness | Tooling supplied with the machine, gap adjustment range, finish of the die lips | Nicked or scratched lips leave a permanent line on every bottle |
| Centring bolts | Make the gap even all round | Adjustable while hot or not, how they lock after adjustment | Parison curls to one side, uneven wall around the bottle |
| Accumulator and push-out ram | Store melt and push it out in one stroke for large parts | Capacity (litres or kg of melt), push-out speed, first-in first-out flow | Melt sits too long and degrades: black specks or brown streaks, inconsistent shot weight |
| Servo die-gap actuator | Moves the mandrel or bushing to the program | Servo type (hydraulic or electric), number of program points, response speed, partial wall control | Wall thickness does not match the setting; walls drift when the zero point shifts |
| Parison cutter | Cuts the parison after the mould closes | Knife type (hot, cold or swing), timing adjustment | Ragged parison end, parison drags on the knife, large neck flash |
3. Mould, clamp and carriage
This unit takes the parison, pinches it and holds the mould shut through blowing and cooling. A shuttle machine slides the mould under the head, collects the parison and returns to the blow station. A double-station machine has two moulds taking turns. A rotary wheel machine carries many moulds on a wheel that turns past the head continuously, for very high volumes.
| Part | Job | What to check on the spec / at acceptance | Symptom when worn or failing |
|---|---|---|---|
| Carriage (shuttle or rotary) | Moves the mould between head and blow station | Stroke, speed, number of stations, centring under the head | Mould off-centre, parison pinched crooked, flash uneven on the two sides |
| Clamp | Pinches off and resists the blow pressure | Maximum clamp force, platen size, daylight, platen parallelism | Incomplete pinch-off weld, thin flash along the parting line, mould opens during blowing |
| Mould | Shapes and cools the part | Mould material and pinch-off material, cooling channels, vents | Blurred surface detail, uneven cooling, warped bottles |
| Pinch-off insert | Cuts and welds the parison end into the bottle base | Hard, replaceable insert; edge angle and land width as recommended by the mould maker | Rounded edge no longer cuts the flash, or too sharp an edge leaves a thin weld that fails the drop test |
| Cooling channels | Pull heat out of the bottle wall | Distance from the cavity surface, separate circuits for neck, body and base, flow per circuit | Scale blocks channels, part of the bottle runs hotter, rocker bottoms, dimensions drift |
| Blow pin or needle | Injects air and calibrates the neck | Pin size to suit the neck finish, air inlet and exhaust valves | Out-of-round necks, heavy neck flash, plastic fragments in the neck |
| Blow air valves | Supply blow air and pre-blow, then exhaust | Adjustable pressure range, valve size, timing settings | Leaks cause incomplete blowing, slow cooling, high shrinkage |
4. Downstream
This section is often overlooked when buying a machine, yet it decides how many bottles actually reach the customer and in what state the flash returns to the hopper.
| Part | Job | What to check on the spec / at acceptance | Symptom when worn or failing |
|---|---|---|---|
| Deflashing / trimming station | Removes neck, base and handle flash | Trimming method (punch, spin or neck cutting), changeover time for the trim tooling | Flash left on, burrs at the neck, bottles dented by the punch |
| Leak tester | Rejects leaking bottles from the line | Test principle (pressure decay is the most common), sensitivity, a reference leaking bottle to test the tester | Leakers reach the customer, or good bottles are rejected |
| Take-out | Transfers bottles from the mould to the next station | Number of axes, travel, adjustment for each mould | Bottles dropped, dented necks |
| Flash conveyor and granulator | Grind flash into regrind and convey it back to the hopper | Granulator screen size, dust removal, return conveying | Regrind full of fines, unsteady feeding, colour or MFI drift |
5. ISBM: the units that differ
ISBM has no parison; it starts from an injection-moulded preform. A single-stage (1-step) machine injects the preform, conditions it and blows it in one machine, using the heat left from injection. A two-stage (2-step) process moulds or buys preforms first, then feeds them to a blow machine with a reheat oven. Both need a stretch rod and two air pressure levels. Drying PET before injection is the job of auxiliary equipment.
| Part | Job | What to check on the spec / at acceptance | Symptom when worn or failing |
|---|---|---|---|
| Preform injection unit (1-step) | Melts PET and injects it into the preform mould | Screw and shot size, preform mould clamp force, number of cavities | Bubbles or haze in preforms, weight variation, high acetaldehyde (AA) when melt stays too long in the barrel |
| Reheat oven | Heats preforms above Tg with infrared (IR) lamps | Number of lamps or zones along the preform, reflectors, power adjustment per zone | A failed lamp or dirty reflector gives thick and thin bands in the bottle wall, pearlescent bottles |
| Preform rotation | Turns preforms through the oven so they heat evenly all round | Rotation speed, preform holder (spindle) | Uneven wall around the bottle |
| Neck cooling | Keeps the preform neck finish from deforming | Heat shields, air or water cooling at the neck | Distorted threads, caps that do not seal |
| Stretch rod | Stretches the preform lengthwise before and during blowing | Stroke, speed, pneumatic or servo drive | Off-centre gate at the base, heavy base |
| Pre-blow and high-pressure blow valves | Low pressure during stretching, then high pressure to form against the mould | Pressure range, valve timing, dead volume in the air lines | Blurred detail, incompletely formed bottles, wasted air |
| HP compressor and air recovery | Supplies blow air and returns part of the exhaust air to pre-blow or the low-pressure network | Pressure and flow against full-line demand, air dryer and oil filters | Pressure drops at full output, water or oil in the air stains bottles |
| Blow mould and base mould | Shape the bottle and base, for example the petaloid base of carbonated drink bottles | Quick mould change, separate base cooling | White, cracked or collapsing bases under pressure |
Machine types
The table compares the main layouts you will meet. Pros and cons are relative to each other, not performance figures.
| Type | Principle | Suits | Strengths | Limits |
|---|---|---|---|---|
| EBM, continuous head, shuttle | Extruder runs continuously; the mould shuttles in to collect the parison | Small to medium bottles and jerry cans | Flexible, easy mould change, several heads for multi-cavity work | On large parts the parison hangs long enough to sag |
| EBM, rotary wheel | Many moulds on a wheel collect the parison continuously | High-volume bottles, one shape, long runs | High output, very steady rhythm | Hard to change over, many mould sets needed |
| EBM, accumulator head | Stores melt, then pushes it out fast in one stroke | 200 L drums, IBCs, automotive parts, heavy parts | Long parisons drop quickly, less sag | Melt dwells in the head, slower colour change, watch for degradation |
| EBM, co-extrusion | Several extruders feed one head to build a multilayer wall | Bottles needing a barrier layer, a regrind or PCR middle layer, a coloured or glossy skin | Each layer does one job; PCR hidden in the middle | Complex head, layer ratios to control, multilayer flash is harder to reuse |
| ISBM, single-stage (1-step) | Injects the preform, conditions and blows it in one machine | Medium volumes, wide-mouth jars, bottles where scuffed preforms are unacceptable | No preform storage, uses the heat from injection | The whole machine is tied to the injection cycle; a changeover means two mould sets |
| ISBM, two-stage (reheat) | Preforms moulded separately, reheated in an IR oven, then blown | Water and carbonated drink bottles at high volume | Fast blow machines; preforms can be bought in | Energy to reheat; oven profile must be kept steady across room temperature and preform lots |
How to size the machine
Do not start from a model name or screw size. Start from the bottle and the hourly volume you need, then work backwards through the machine one unit at a time.
- Start with the part Volume, weight, height, maximum width, handle, material and annual volume. This decides EBM or ISBM, continuous or accumulator head, and how many cavities.
- Work out extruder output Required output (kg/h) = (bottle weight + flash weight) × cavities × cycles per hour. Weigh the real flash from a trial mould, because flash is a significant share of an EBM shot. Then choose an extruder that delivers this output at a melt temperature low enough for a blow grade, not at maximum screw speed.
- Die head size Parison diameter relates to bottle size through the blow-up ratio (maximum bottle width ÷ parison diameter). Typical EBM work sits around 2:1 to 4:1; the higher the ratio, the thinner the corners and edges. For handled bottles, choose a die size that lets the parison cover the handle area.
- Continuous or accumulator head If the parison is so long and heavy that it sags while hanging, use an accumulator head that pushes it out quickly. Accumulator capacity must exceed the shot weight (bottle plus flash) but should not be far larger, or melt will dwell too long.
- Clamp force Clamp force must exceed the force with which the blow air pushes the mould apart, plus the force needed to pinch off. Air force = blow pressure × projected area of the part on the parting plane. A unit-conversion example: 6 bar = 0.6 N/mm²; with a projected area of 1,000 cm² (100,000 mm²) the air force is 60 kN, about 6 tonnes, before adding pinch-off force, which depends on pinch-off length and parison thickness. Have the machine or mould maker confirm the figure.
- Platen size and daylight All cavities must fit on the platen, the opening stroke must release the deepest bottle, and the distance from head to mould must suit the parison length.
- Compressed air EBM commonly blows at around 3–10 bar; ISBM uses pre-blow at around 5–12 bar and high-pressure blow at around 25–40 bar. Air per cycle can be estimated from the volume of all cavities plus line dead volume, multiplied by the ratio of absolute blow pressure to atmospheric pressure. Use that to check compressor and receiver size.
- Cooling capacity The heat the chiller must remove depends on the plastic throughput per hour and the temperature drop. HDPE is highly crystalline, so the latent heat of crystallisation has to be removed as well. Cooling is usually the longest step in the cycle; have the machine maker size the chiller from the real bottle.
Typical reference range — confirm with the machine maker and the TDS.
Maintenance checkpoints
The intervals are a starting point. Adjust them to the maker's manual, running hours and materials. Lines running a lot of regrind or PCR usually need more frequent screen and head checks.
| Interval | Checkpoint | What to look at | What happens if skipped |
|---|---|---|---|
| Every shift | Safety gates, interlocks, emergency stops | Opening a gate really stops the mould and carriage; light curtains work | Someone is trapped by the mould or hit by high-pressure air |
| Every shift | Parison and die lips | Curling, lines, black specks, change in parison length | A whole lot of bottles is scrapped before anyone notices |
| Every shift | Leak tester | Insert the reference leaking bottle; the tester must reject it | Leakers reach the customer |
| Every shift | Air pressure and cooling water | Blow pressure, water in and out temperatures, leaks | Incompletely blown bottles, rocker bottoms, dimensions drift |
| Weekly | Die lips | Clean deposits with brass or copper tools, never steel scrapers | Scratched lips and a permanent line on every bottle |
| Weekly | Blow pin and cutter | Wear, stuck flash, knife sharpness | Out-of-round necks, ragged parison ends |
| Weekly | Mould vents and surfaces | Deposits in the vents | Blurred detail, trapped-air marks on bottles |
| Weekly | Compressor condensate and air dryer | Auto drains working, dryer running to its setting | Water in the air, stained bottles, valves wear fast |
| Weekly (ISBM) | IR lamps and reflectors | Failed lamps, hazy or dirty reflectors | Thick and thin bands in the bottle wall, pearlescent bottles |
| Monthly | Pinch-off edges | Measure land width, look for chips or rounding | Flash does not separate, or a weak base weld that fails the drop test |
| Monthly | Die-gap actuator zero | Check servo zero and stroke against the setting | Wall thickness drifts with an unchanged program |
| Monthly | Cooling water quality and flow per circuit | Scale, hardness, water treatment, strainers | Blocked mould channels, uneven cooling, longer cycles |
| Monthly | Heater bands and thermocouples | Current per band, readings against a reference instrument | Real temperature differs from the screen; sag or unmelted material |
| Monthly | Hydraulic oil | Level, temperature, filters | Sticky servo valves, inconsistent clamp force |
| Yearly | Screw and barrel | Measure flight diameter and barrel bore against new values | Lower output, higher melt temperature, poor colour mixing |
| Yearly | Complete head | Strip and clean, inspect flow-channel surfaces, seals and bolts | Degraded hold-up, recurring black specks, slow colour change |
| Yearly | Air receivers and safety valves | Inspect per pressure-vessel regulations and the maker's manual | Hazard from high-pressure vessels |
| Every repair | Lock-out/tag-out | Isolate heaters and motors; release hydraulic pressure, hydraulic accumulators and compressed air before approaching; wear heat-resistant gloves and a face shield when purging | Electric shock, crushing by the mould, burns from the parison or from melt spurting out of the head |
Masterbatch and additives on this machine
On an EBM machine, masterbatch enters at the extruder throat through a dosing unit mounted on the hopper. A blow molding extruder is a single screw and mixes far less than a twin-screw compounder, so colour consistency depends on three things: an MB carrier that melts like the base resin, a screw with a mixing section, and steady feeding. On an ISBM machine, additives go in at the preform injection unit, because the blowing step does not remelt the material.
- Flash regrind loops back Ground flash already contains colour and additive. Calculate the let-down on the virgin portion and keep the regrind ratio constant, or colour and additive level in the bottle will swing with the amount of flash.
- Colour streaks on bottles If colour runs in lengthwise streaks, check feeding and mixing before blaming the MB. See color streaks.
- Black specks and gels More often come from degraded hold-up in the head or accumulator, or a broken screen, than from the MB. See black specks and gels.
- Sharkskin surface appears when shear stress at the die lips is too high. A processing aid (PPA) can help, but check temperatures and the condition of the lips first. See melt fracture.
- UV for jerry cans, water tanks and chemical containers stored outdoors. See plastics cracking in sunlight.
- Antistatic for bottles that collect dust on the shelf. See parts attracting dust.
- Cost per good bottle including scrap and regrind: use the cost-in-use calculator.
Machine problems cannot be fixed with additives: a worn screw that no longer melts fully, scratched die lips, an off-centre die gap, worn pinch-off edges or blocked mould channels. Repair the machine first, then tune the formulation. ACS designs masterbatch formulations to suit the user's base resin and machine; if you are not sure which side the problem sits on, send us photos of the bottle.
Related process articles
For the blowing cycle, the parameters to control and the resin grades from the process side, read Blow molding. Defects tied directly to the blow molding machine: melt fracture · gels · black specks · color streaks
FAQ
Blow molding machine questions we hear often
What should I check when buying a used blow molding machine?
Ask for a run with resin and a mould close to your real job, and see whether output reaches the spec at a normal melt temperature. Measure the screw and barrel, inspect the die lips for damage, run a parison program and confirm the wall thickness really follows it. Check platen parallelism, hydraulic leaks and the servo repair history. For ISBM, look at the IR lamps, reflectors and the running hours of the high-pressure compressor.
How can I tell the screw or the head is wearing?
A worn screw usually shows as lower output at the same screw speed, a higher melt temperature and colour that no longer mixes as well. Confirm by measuring flight diameter and barrel bore against new values. A head with problems gives lengthwise lines in the same position on every bottle, one thin side, or black specks that do not clear after purging. If the symptom stays in the same place after a change of resin lot, the cause is usually the machine.
Continuous or accumulator head: how do I choose?
Look at parison weight and length. Small to medium bottles and jerry cans run well on a continuous head, with fast colour changes and no melt hold-up. Heavy, long parts such as 200 L drums or IBCs need an accumulator head, because the parison must drop quickly before it sags. The trade-off is longer melt dwell in the head, slower colour changes and more attention to degradation.
How do I make colour changes faster on a blow molding machine?
Going from light to dark is faster than the reverse. Clear regrind of the old colour from the hopper and dosing unit first, purge with a purging compound or virgin resin, then run until the colour has fully changed. Accumulator heads take longer than continuous heads because they hold more melt. If streaks of the old colour persist for a long time, there is usually a dead spot in the head flow channels and the head needs to be stripped and cleaned.
Caution
General knowledge for understanding only. Numbers are typical reference ranges. Selection, installation, operation and maintenance must follow the machine maker's manual and instructions and your plant's safety rules.